01
Liquid Cooling Cold Plates
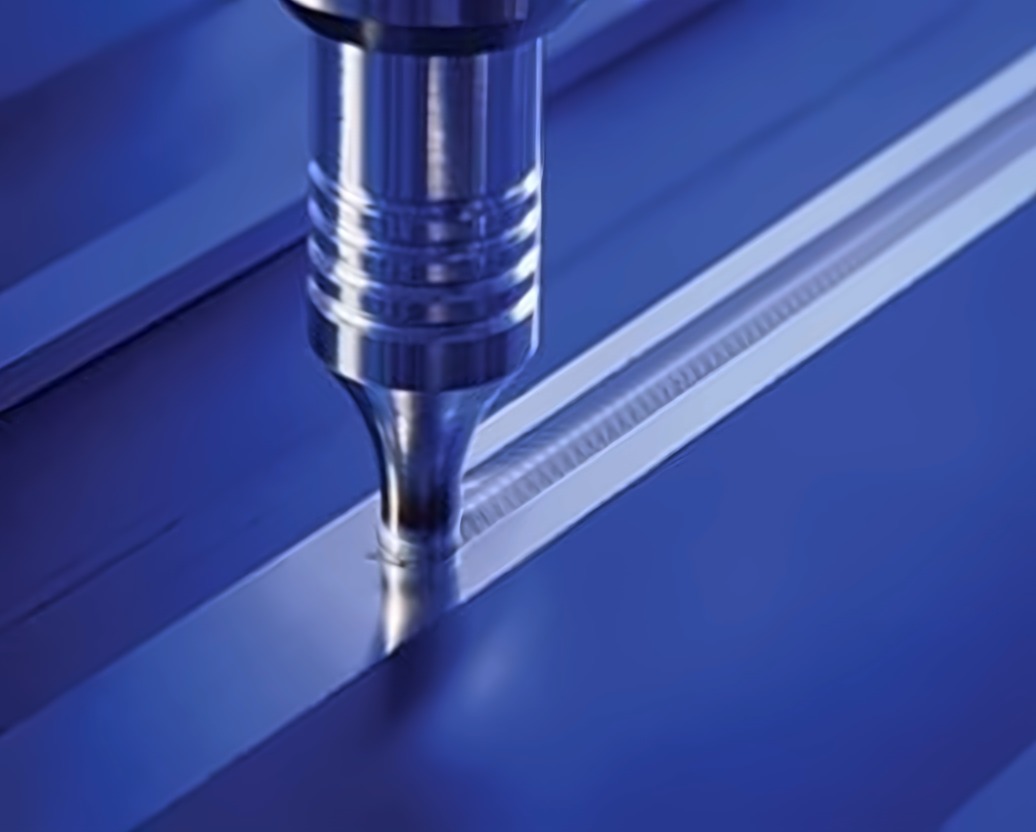
Machined or extruded channel plate with an FSW closure, the core architecture.
Home / Industries / Thermal Structures
Liquid cooling assemblies fail where they are joined. LeapFast builds cold plates and heat exchangers as a machined or extruded channel plate with a friction stir welded closure, a hermetic, full-strength joint with no braze foil, no gasket, and no leak path.
Primary capability
As power density rises, brazed and gasketed cooling designs run out of room, thermally and in yield. A friction stir closure seals hermetically, survives pressure cycling, and removes an entire furnace step from the build. It also permits channel geometry that a brazed stack-up cannot hold.
The problem
Applications
01
Machined or extruded channel plate with an FSW closure, the core architecture.
02
A brazed-plate replacement with a hermetic, full-strength seal.
03
Structural, sealed enclosures with integral cooling.
04
Inverter and drive thermal structures at rising power density.
Also relevant here
ALSO
Aluminum-to-copper joints that remove bulky mechanical transitions and let the designer pick the right alloy for each side.
ALSO
Weld parameters modeled and optimized before metal is cut, which shortens qualification.
Why us
Questions
A friction stir closure is a solid-state joint with parent-metal-class strength and a hermetic seal, produced without a furnace cycle. Brazing adds a thermal cycle, fixturing, and a joint whose integrity depends on wetting.
Usually the channel design can stay and only the closure changes, which is the least disruptive way to trial the process. Send a drawing and we will tell you.
Development and prototype now, with production scaling through equipment and university partners. Tell us the volume and the date and we will be straight with you about the ramp.
Next step
A drawing, a STEP file, or a sketch and a size is enough. We reply within 3 business days, including when the answer is no.